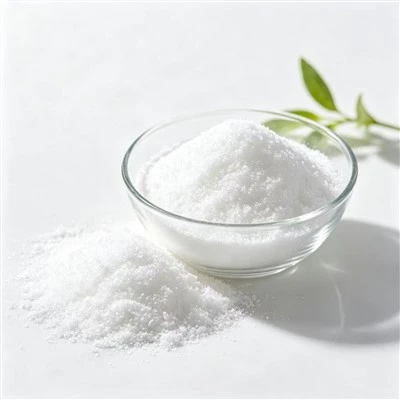
This high-purity, food-grade steviol glycoside is derived exclusively from premium natural stevia leaves and stems. It is produced using a comprehensive, modern, and eco-friendly process that includes purely physical low-temperature extraction, multi-stage resin adsorption and separation, high-precision decolorization and purification, aseptic concentration, and spray drying. The entire production process is free from synthetic chemical sweeteners, preservatives, fluorescent whitening agents, and harmful solvents, making it a truly natural, zero-calorie, plant-based sugar substitute.
This product offers a sweetness level 200–300 times that of ordinary sucrose while being virtually calorie-free. It does not raise blood sugar levels, contribute to weight gain, or cause insulin fluctuations, aligning perfectly with global healthy eating trends. The powder features uniform fineness, high bulkiness, and excellent flowability; it does not clump or adhere to vessel walls, ensuring high compatibility across various applications-including liquid beverage formulation, dry powder blending, high-temperature baking, sauce preparation, and the manufacture of solid dietary powders. Produced under strict international food-grade standards, the product ensures consistent quality across batches and is suitable for long-term, large-scale export to markets in Europe, the Americas, Southeast Asia, the Middle East, and Africa. We support customer sample testing, formula optimization, and long-term partnerships involving regular full-container orders.
Product Basic Specifications Table
| Physical Appearance Specifications | |
| Appearance | Pure white, fine powder; fluffy, free-flowing, and free of hard clumps or granules. |
| Color | Uniformly bright white throughout; free of yellowing, graying, black specks, or foreign impurities. |
| Odor | Clean, sweet, herbal aroma; free of burnt, musty, solvent, or bitter off-notes. |
| Fineness | Standard 80 mesh; customizable to 100 or 120 mesh (ultra-fine) for faster dissolution. |
| Key Active Ingredient Specifications | |
| Total Steviol Glycosides | Various specifications available (90%–98%); purity customizable to client requirements. |
| Rebaudioside A (RA) Content | Adjustable range of 40%–97%; high-RA grades offer reduced bitterness and a taste profile closer to white sugar. |
| Sweetness Intensity | 200–300 times that of sucrose; high-purity grades offer a cleaner sweet taste without off-flavors. |
| Moisture and Stability Specifications | |
| Moisture Content | ≤5.0%; low hygroscopicity ensures resistance to clumping or moisture absorption during long-distance sea transport and extended storage. |
| pH Value (1% aqueous solution) | 4.5–7.0; compatible with a wide range of pH environments. |
| Thermal Stability | Stable at high processing temperatures (120°C) within a pH range of 3.0–10.0; no decomposition, loss of sweetness, off-flavors, or solution turbidity. |
| Solubility | Rapid and complete dissolution in cold, warm, and boiling water; the resulting solution is clear and transparent, free of flocculation, sediment, or separation. |
| Nutritional Characteristics | |
| Caloric Value | Virtually 0 kcal/g; provides no absorbable calories. |
| Glycemic Index (GI) | ≈0; does not trigger blood sugar fluctuations; free of sucrose, fructose, and glucose. |
| Carbohydrates | Trace amounts; does not contribute to fat accumulation in the body. |
| Target Consumers | Suitable for individuals managing sugar intake, diabetics, those seeking fat loss, children, and fitness enthusiasts. |
| Safety and hygiene limit indicators (compliant with export standards for Europe, the US, and Southeast Asia) | |
| Heavy metal limits | Lead (Pb) ≤1.0 mg/kg Arsenic (As) ≤0.5 mg/kg Mercury (Hg) ≤0.1 mg/kg Cadmium (Cd) ≤0.3 mg/kg |
| Residual solvents | Free from ethanol, methanol, and extraction solvent residues; utilizes a purely physical extraction process. |
| Pesticide residues | All pesticide residue levels are below the EU's limits for food ingredients. |
| Microbiological indicators | Total aerobic microbial count: ≤1000 CFU/g Molds and yeasts: ≤100 CFU/g Escherichia coli: Not detected Salmonella, Staphylococcus aureus, and pathogenic bacteria: Not detected |
| Additive | Free from artificial colors, artificial flavors, preservatives, and bleaching agents. |
Core Product Advantages (Comprehensive Details)
We source raw materials exclusively from large-scale, standardized stevia plantations. The plants benefit from natural sunlight during growth and are free from the risk of excessive pesticide residues. Post-harvest processing involves washing, sorting, and impurity removal, retaining only the stems and leaves that provide the desired sweetness. The entire process utilizes pure water extraction, physical purification, and aseptic drying-free from chemical modification or artificial additives. Finished products surpass international food safety standards regarding heavy metals, pesticide residues, and microbial counts. Free from banned additives and irritating impurities, this product is the premier choice for high-end overseas health foods, maternal and infant products, functional dietary supplements, and sugar-free health products. It easily passes customs quality inspections worldwide, ensuring zero-risk clearance.
The ultra-high sweetness of these steviol glycosides allows manufacturers to achieve excellent results with minimal dosage. Compared to white sugar, the required amount is merely 1/200 to 1/300 to achieve the same level of sweetness. This drastically reduces raw material procurement weight, warehouse storage requirements, packaging material consumption, and logistics costs.
Unlike ordinary sugar substitutes-which often suffer from a harsh, one-dimensional sweetness and a bitter aftertaste-this product offers a clean, mellow sweetness profile closely resembling the natural, crisp taste of sucrose. It delivers a premium mouthfeel when used alone and, when blended with polyols like erythritol, xylitol, maltitol, or fructose-glucose syrups, perfectly replicates the rich flavor profile of sucrose. This significantly elevates the sensory quality of the final product and boosts consumer repurchase rates.
Many natural sweeteners on the market suffer from limitations such as heat sensitivity, degradation in acidic environments, loss of sweetness during sterilization, and issues like discoloration or cloudiness, all of which severely constrain production processes. In contrast, this steviol glycoside product is highly resistant to heat, acids, alkalis, and prolonged sterilization. It maintains a stable molecular structure-without degrading, losing sweetness, turning bitter, or discoloring-across a wide pH range (3–10) and under high-temperature processing conditions (up to 120°C). It is suitable for a wide range of industrial processes, including high-temperature flash pasteurization for beverages, prolonged boiling for jams, high-temperature baking for biscuits and bread, high-temperature drying for powders, and high-pressure sterilization. It dissolves rapidly in cold, warm, or hot water, yielding a clear, transparent solution free from suspended matter, sediment, or phase separation. It is compatible with high-speed automated production lines, ensuring no pipeline clogging and maintaining system stability.
As consumer demand for low-sugar, sugar-controlled, fat-reducing, and blood-sugar-regulating products surges, traditional sucrose and high-fructose corn syrup are increasingly being replaced due to their high caloric content, high glycemic index, and tendency to cause weight gain and metabolic issues. Steviol glycosides offer zero calories, a zero glycemic index, zero fat, and zero carbohydrates; they do not interfere with human blood sugar metabolism and do not contribute to caloric surplus or fat accumulation.
It is suitable for diabetics, fitness enthusiasts, those seeking weight loss or sugar control, and children on low-sugar diets. It serves as a core, essential ingredient for overseas sugar-free beverages, zero-calorie snacks, low-sugar baked goods, functional meal replacements, sugar-control dietary powders, and health-oriented foods. It enables clients to precisely position their products in the premium health market, thereby enhancing product value and market competitiveness.
Produced using an advanced spray-drying granulation process that precisely controls moisture content and powder structure, the product is loose, dry, and uniform in particle size, with high resistance to moisture absorption and caking. When stored long-term in a cool, dry environment at ambient temperature, it remains free from issues such as moisture-induced caking, discoloration, off-flavors, or loss of efficacy.
Export packaging utilizes thickened food-grade paper-plastic bags with a double-layer PE waterproof liner. This provides superior sealing against moisture, contamination, and damage, making it fully suitable for long-distance cross-border transport via sea, land, or air. Classified as general food cargo, it requires no cold chain, hazardous material qualifications, or special storage conditions, significantly reducing overall storage and logistics costs for overseas clients.


Hot Tags: stevia extract stevioside powder, China stevia extract stevioside powder manufacturers, suppliers, factory, Erythritol Raw Powder, food additive raw materials, L Arabinose Raw Powder, Lactic Acid Bacteria Powder, Pure Trehalose Powder, Vitamin B2 Raw Powder